
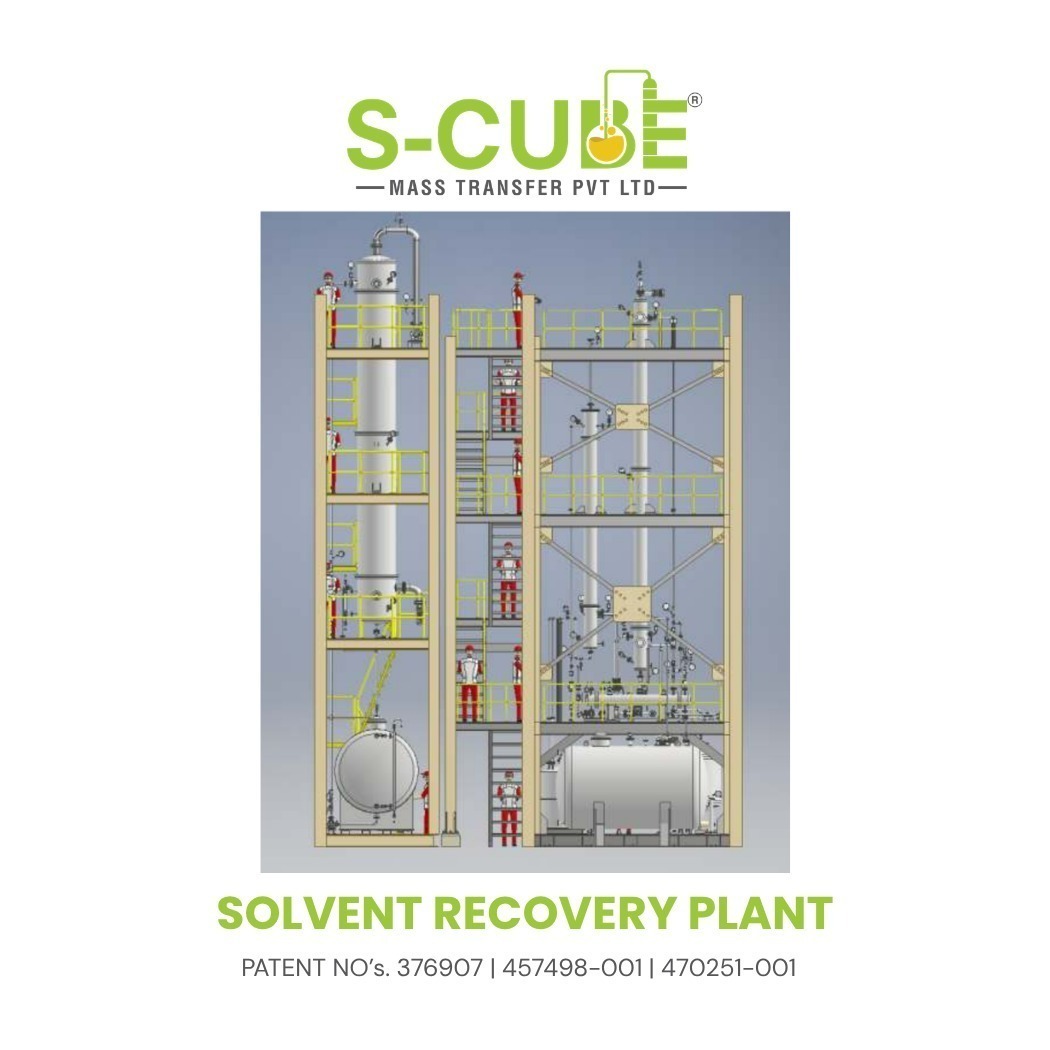
A Solvent Recovery Plant Manufacturer in Hyderabad must evaluate the physical and thermodynamic properties of the process stream before determining the appropriate recovery configuration. Solvent recovery is primarily a separation-engineering requirement, and equipment selection should be based on feed composition, volatility, purity targets, recovery requirements, and operating conditions.
S-Cube Mass Transfer Pvt. Ltd. provides solvent recovery systems for pharmaceutical, chemical, specialty chemical, petrochemical, coating, and other process industries where solvent-bearing streams require separation and recovery.
Distillation is commonly applied where components have sufficient differences in volatility. However, the required process configuration depends on relative volatility, vapour-liquid equilibrium, azeotropic behaviour, contaminants, thermal stability, and required recovered-solvent quality.
Operating pressure is another important consideration. Vacuum operation may be evaluated for heat-sensitive materials or where lower operating temperatures are required. The selected pressure affects vapour volume, column hydraulics, condenser duty, reboiler duty, and equipment dimensions.
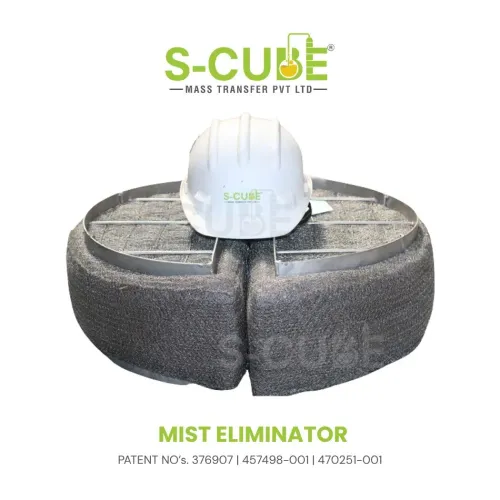
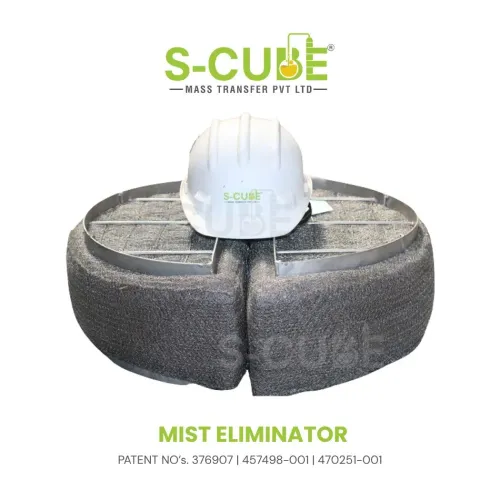
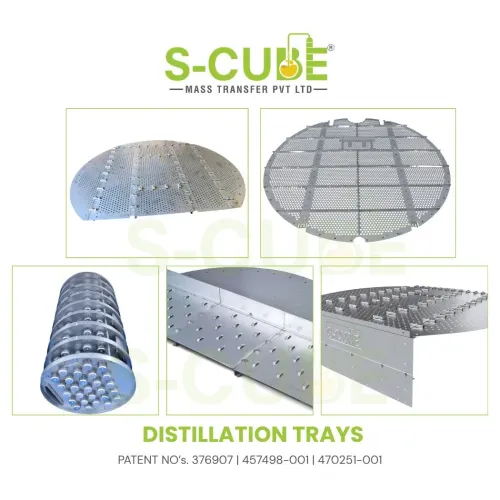
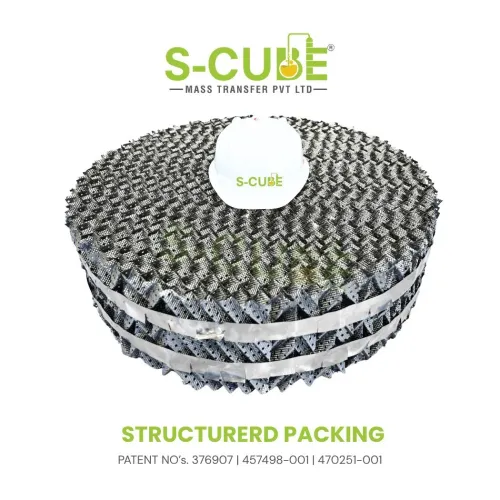
Mass-transfer equipment such as packing, trays, distributors, collectors, and mist eliminators should be selected according to process and hydraulic conditions. Pressure drop becomes particularly relevant in vacuum systems.
Material of construction should be compatible with the solvent mixture and expected contaminants while meeting operating temperature, pressure, and project requirements.
Industrial facilities in Hyderabad evaluating solvent recovery can provide S-Cube Mass Transfer Pvt. Ltd. with feed composition, throughput, recovery target, purity requirement, and utility information for technical assessment.