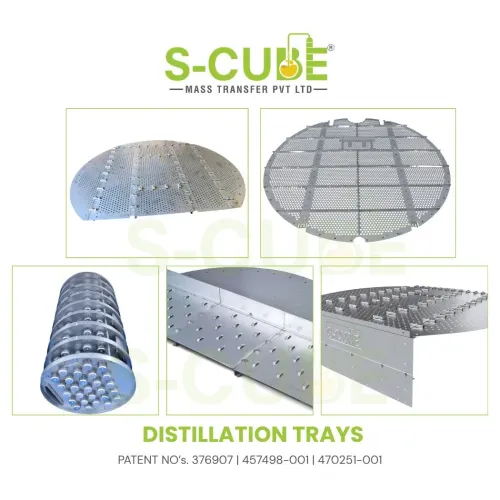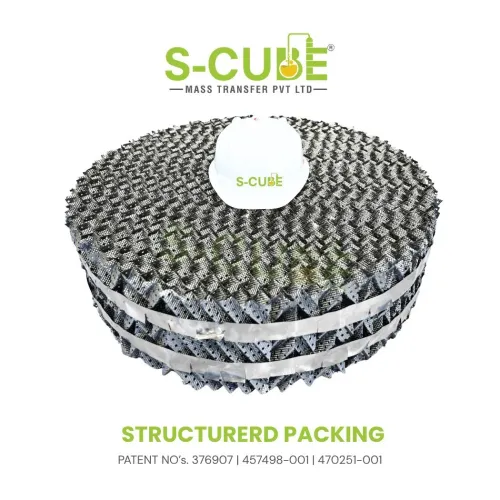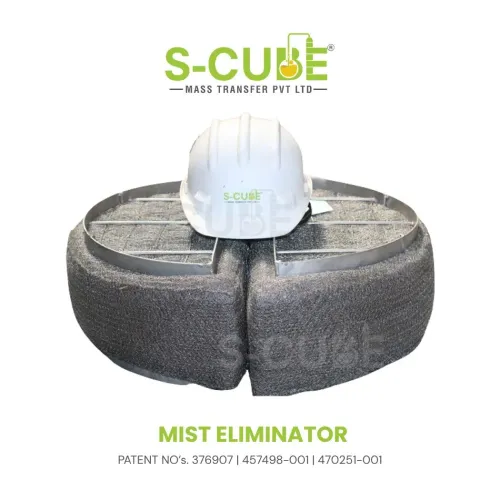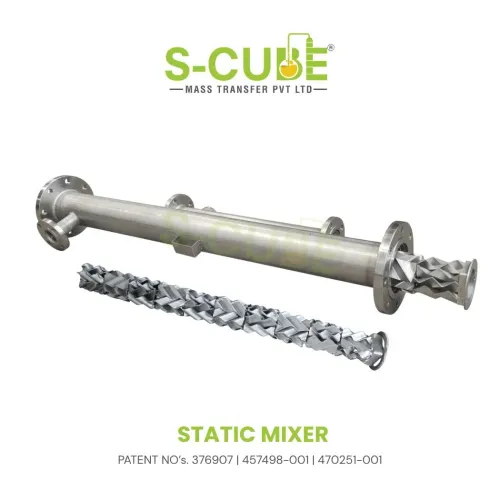

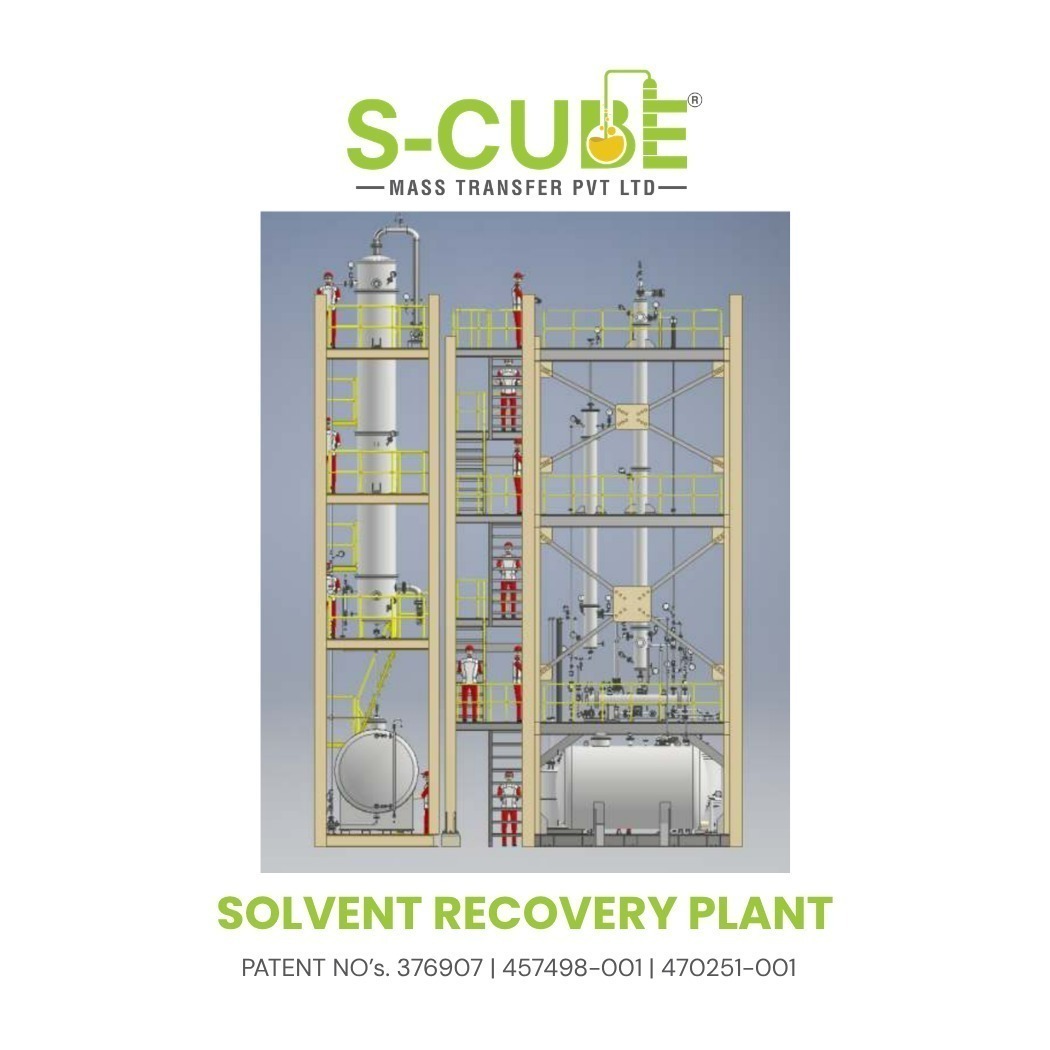
A Solvent Recovery Plant Supplier in Hyderabad should establish technical feasibility based on the characteristics of the solvent-bearing stream and the required recovered product. Recovery performance cannot be assessed solely from feed volume because composition and thermodynamic behaviour determine the achievable separation.
S-Cube Mass Transfer Pvt. Ltd. supplies solvent recovery systems for chemical, pharmaceutical, API, specialty chemical, petrochemical, coating, and other industrial applications.
The initial process assessment should consider solvent identity, concentration, impurities, feed quantity, required recovery percentage, recovered-solvent purity, operating schedule, temperature sensitivity, available utilities, and materials of construction.
Conventional distillation can be suitable when adequate volatility differences exist between the components. For mixtures with close boiling points, azeotropic behaviour, thermal sensitivity, or complex contaminants, the process configuration requires further engineering assessment.
Column hydraulics are also significant. Vapour and liquid loading, flooding limits, pressure drop, packing characteristics, distributor performance, and operating turndown can affect separation performance. For vacuum operation, controlling pressure drop throughout the column and associated equipment becomes particularly important.
Material selection should address solvent compatibility, corrosion potential, design temperature, operating pressure, mechanical requirements, and applicable project specifications.
Chemical and pharmaceutical manufacturers in Hyderabad evaluating solvent recovery systems can provide S-Cube Mass Transfer Pvt. Ltd. with representative feed data, required capacity, recovery objectives, purity specifications, and utility conditions for a detailed technical evaluation.